

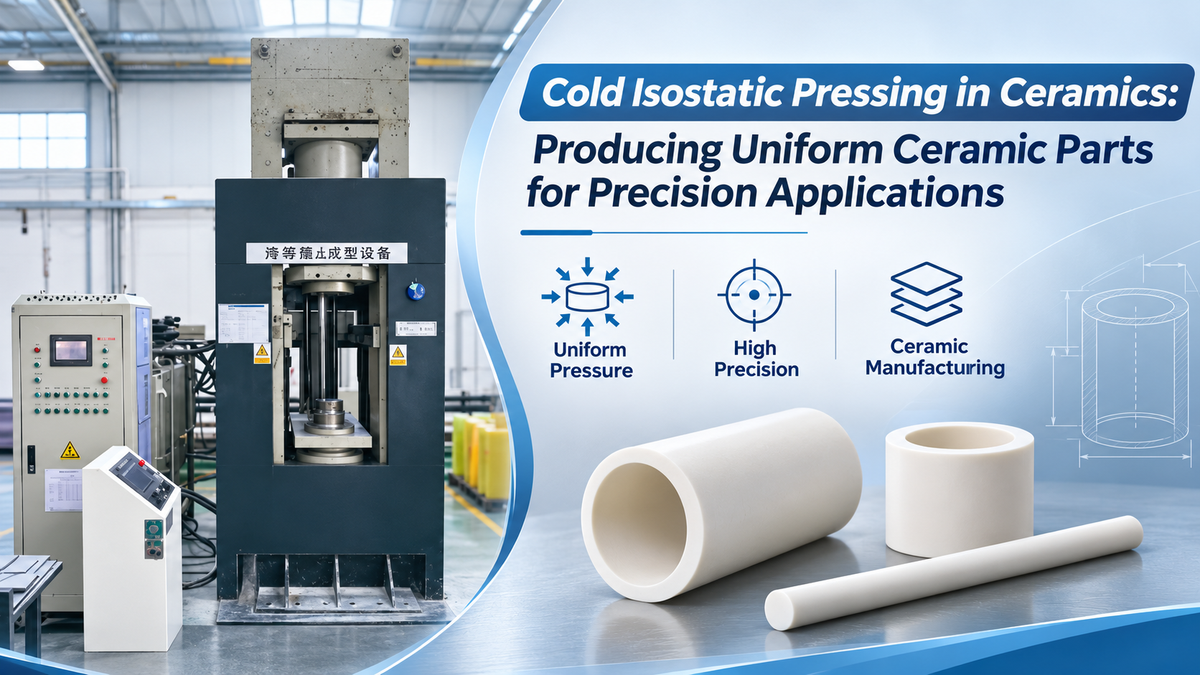
Ceramic materials are known for high hardness, wear resistance, corrosion resistance, electrical insulation, and ability to withstand high temperatures. They are widely used in semiconductors, automotive, medical, electronics, and industrial equipment.
However, manufacturing ceramic parts is not always easy. If ceramic powder is not distributed evenly during forming, it can lead to uneven shrinkage, dimensional changes, internal cracks, or even part failure.
Cold Isostatic Pressing (CIP) is a forming process that uses liquid pressure to compact ceramic powder evenly from all directions to help reduce these problems.
As a trusted custom ceramic parts manufacturer, XY-GLOBAL has over 15 years of experience in precision ceramic manufacturing, delivering precision ceramic components with consistent quality. Send us your cold isostatic pressing ceramic part drawings and requirements. Our engineering team will provide free DFM support and help you find a suitable, cost-effective manufacturing solution.
What Is Cold Isostatic Pressing?
Cold isostatic pressing is a powder compaction process that uses liquid pressure to press materials into shape. It is usually carried out at room temperature.
Unlike conventional uniaxial pressing, CIP places ceramic powder inside a flexible rubber or polymer mold. The mold is then placed in a high-pressure vessel filled with liquid. Pressure is transferred evenly from all directions, compacting the powder inside.
Typical operating pressures range from 100 to 600 MPa, depending on the ceramic material, powder characteristics, part size, and equipment capacity.
CIP cold isostatic pressing is another search term used to refer to the same process, which is commonly abbreviated as CIP.
Compared with uniaxial pressing in a rigid mold, CIP helps reduce density differences caused by friction between the powder and mold walls. This is particularly useful for long rods, ceramic tubes, thick-walled parts, and large ceramic blanks.
It is important to note that CIP produces a ceramic green body, not a finished, sintered part. Further processing, such as sintering, dimensional machining, and surface finishing, is usually required.

How Does the Cold Isostatic Pressing Process Work?
A complete cold isostatic pressing process includes powder preparation, mold design, filling, sealing, pressurization, pressure holding, decompression, and subsequent sintering.
Ceramic Powder Preparation
Powder quality has a direct impact on the final forming results. Common ceramic materials include Alumina (Al₂O₃), Zirconia (ZrO₂), Silicon Carbide (SiC), etc.
Raw ceramic powder usually may have a particle size ranging from 0.1 to 10 μm. For powders that need better flowability and mold filling, spray drying can be used to produce granules, typically around 50–150 μm.
Particle size distribution, particle shape, bulk density, and flowability all affect the compaction results. If the powder is not filled evenly, applying the same external pressure does not necessarily produce the desired green density.
Flexible Mold Design and Filling
Ceramic powder is placed into a flexible mold. The mold is usually made of rubber or polyurethane and must have enough elasticity, strength, and sealing capability to withstand high pressure.
The mold determines the basic shape of the compacted part. For ceramic tubes, rods, and components with center holes, a mandrel or other supporting structure can also be used.
During filling, it is important to keep the powder evenly distributed and minimize trapped air. For parts with higher density requirements, vacuum de-airing may also be used to reduce the effect of trapped air on compaction quality.
Pressurization and Compaction
After filling and sealing, the flexible mold is placed inside a high-pressure vessel. Pressure is then gradually increased through a liquid medium.
Common pressure media include water, water-oil mixtures, and other suitable liquids. The liquid transfers pressure evenly to the mold, compacting the ceramic powder from all directions.
As the pressure increases, ceramic particles rearrange, come into closer contact, and become more tightly packed. The spaces between particles gradually decrease. At higher pressures, some brittle ceramic particles may also break, allowing them to pack more closely.
After reaching the target pressure, the ceramic material is held under pressure for a suitable period. The required time depends on the material and part geometry.
Controlled Decompression and Demolding
Decompression is also an important part of the cold isostatic pressing process.
When external pressure is released, the ceramic green body undergoes some elastic springback. If the pressure is released too quickly, trapped air inside the compact may expand and cause cracks or other defects.
For this reason, decompression speed needs to be controlled, especially for large, thick-walled, or unevenly shaped ceramic parts.
After decompression, the flexible mold is removed and the green body is taken out. Its appearance, dimensions, and overall condition are checked. Green density may also be measured when needed to assess its suitability for the next sintering stage.
Green Machining and Sintering
After CIP, the ceramic green body has some strength, but it has not yet reached its final properties.
Depending on the part design, green machining can be carried out before sintering. This may include trimming the outer shape, machining certain holes, or removing excess material. Since green bodies have limited strength, clamping force and cutting conditions must be carefully controlled to avoid cracks.
The parts then go through high-temperature sintering. As the temperature increases, ceramic particles bond together and the material becomes denser. Porosity decreases, and the ceramic gradually develops its final hardness, strength, and other required properties.
Ceramic parts also shrink during sintering. For some ceramic materials, linear shrinkage can reach approximately 10%–25%. The actual rate depends on the material formulation, initial green density, and sintering conditions. Mold design and green body dimensions must account for this shrinkage in advance.
For parts with tight dimensional tolerances or high surface finish requirements, additional processes may be used after sintering. These include CNC machining, precision grinding, lapping, and polishing.
Wet Bag vs Dry Bag Isostatic Pressing
Cold isostatic pressing mainly uses two methods: Wet Bag Isostatic Pressing and Dry Bag Isostatic Pressing.
The main difference is how the flexible mold is installed and how the powder is loaded.

Wet Bag Isostatic Pressing
Wet bag pressing uses a separate flexible mold. The powder is filled and sealed inside the mold outside the pressure vessel. The entire mold is then placed into the vessel for pressing.
This method offers greater flexibility in mold design and can handle different part sizes and shapes. It is commonly used for product development, small-batch production, large ceramic blanks, and special geometries.
However, loading and unloading the molds takes more time, and the production process is generally less automated than dry bag pressing.
Dry Bag Isostatic Pressing
In dry bag pressing, the flexible mold is fixed inside the pressure vessel. The pressure medium acts on the outside of the mold, while the powder is loaded and the finished compact is removed through dedicated filling and demolding structures.
This design is easier to automate and can achieve shorter production cycles. Depending on the part size and equipment configuration, some industrial systems can complete a pressing cycle in approximately 10–100 seconds.
Dry bag pressing is more suitable for relatively regular shapes, such as cylindrical, tubular, and rod-shaped parts. It is particularly useful for industrial products that require consistent, repeatable production.
However, the fixed mold limits the available part shapes and sizes. The design still needs to be evaluated for each application.
Advantages of Cold Isostatic Pressing
The main advantage of cold isostatic pressing is its uniform pressure distribution. But its benefits go beyond the pressing stage. It can also affect subsequent sintering and the quality of the final ceramic part.
More Uniform Green Density
Uniform pressure helps reduce density differences within the ceramic green body. This lowers the risk of uneven shrinkage during sintering.
It is particularly important for thick-walled, large, and high-aspect-ratio ceramic parts.
Better Green Strength
CIP produces green bodies with good handling strength, making them easier to handle, machine, and move to the sintering stage.
Better green strength also helps reduce damage during handling.
Suitable for Large and Thick-Walled Parts
Compared with some conventional uniaxial pressing methods, CIP is better suited to producing large, thick-walled, and high-aspect-ratio ceramic blanks.
This is particularly useful for ceramic rods, tubes, sleeves, and larger structural components.
Reduced Density-Related Defects
With proper control of powder filling, pressing, and decompression, CIP can help reduce uneven density, internal cracks, and other forming defects.
A more uniform green body also helps improve consistency during sintering.
Flexible Mold Design
Flexible molds can be designed to suit different part geometries. This reduces the need to rely entirely on complex rigid tooling, as is often the case with conventional dry pressing.
Wet bag pressing is particularly useful when different sizes or special shapes are required.
Limitations of Cold Isostatic Pressing(CIP)
Although CIP offers several advantages, it is not the best choice for every ceramic part.
Lower Dimensional Accuracy Before Finishing
Flexible molds can deform under high pressure, and the compact may experience elastic springback after demolding. As a result, the dimensional accuracy and surface finish of CIP green bodies may not match those achieved through precision injection molding or rigid-die pressing.
If a part has tight hole-position tolerances, critical fitting dimensions, or strict surface finish requirements, additional machining is usually needed.
Additional Sintering and Machining Costs
CIP only compacts the powder. It does not directly produce a finished ceramic part.
Sintering, CNC machining, grinding, and polishing can all add to the manufacturing cost. When comparing quotations, it is important to consider the complete manufacturing process rather than the pressing cost alone.
Longer Production Cycle in Some Applications
Wet bag pressing requires separate mold filling, sealing, loading, and demolding operations. Production efficiency can be affected by the amount of manual work involved.
For large-volume, repeat production, dry bag pressing or another automated forming method may be more suitable.
Limited Geometry for Complex Parts
CIP can produce ceramic blanks in various sizes and cross-sections, but flexible molds are not suitable for every complex design.
For parts with small holes, complex internal channels, thin walls, or detailed 3D features, CIM usually offers greater design flexibility.
Powder Preparation Is Critical
Even when pressure is distributed evenly, poor powder particle size control, granulation, filling, or air removal can still cause internal defects.
CIP depends not only on equipment pressure but also on consistent powder preparation and process control.
What Ceramic Parts Can Be Made by Cold Isostatic Pressing?
Cold isostatic pressing ceramics is mainly used for products that require uniform compaction, larger dimensions, or higher green density.
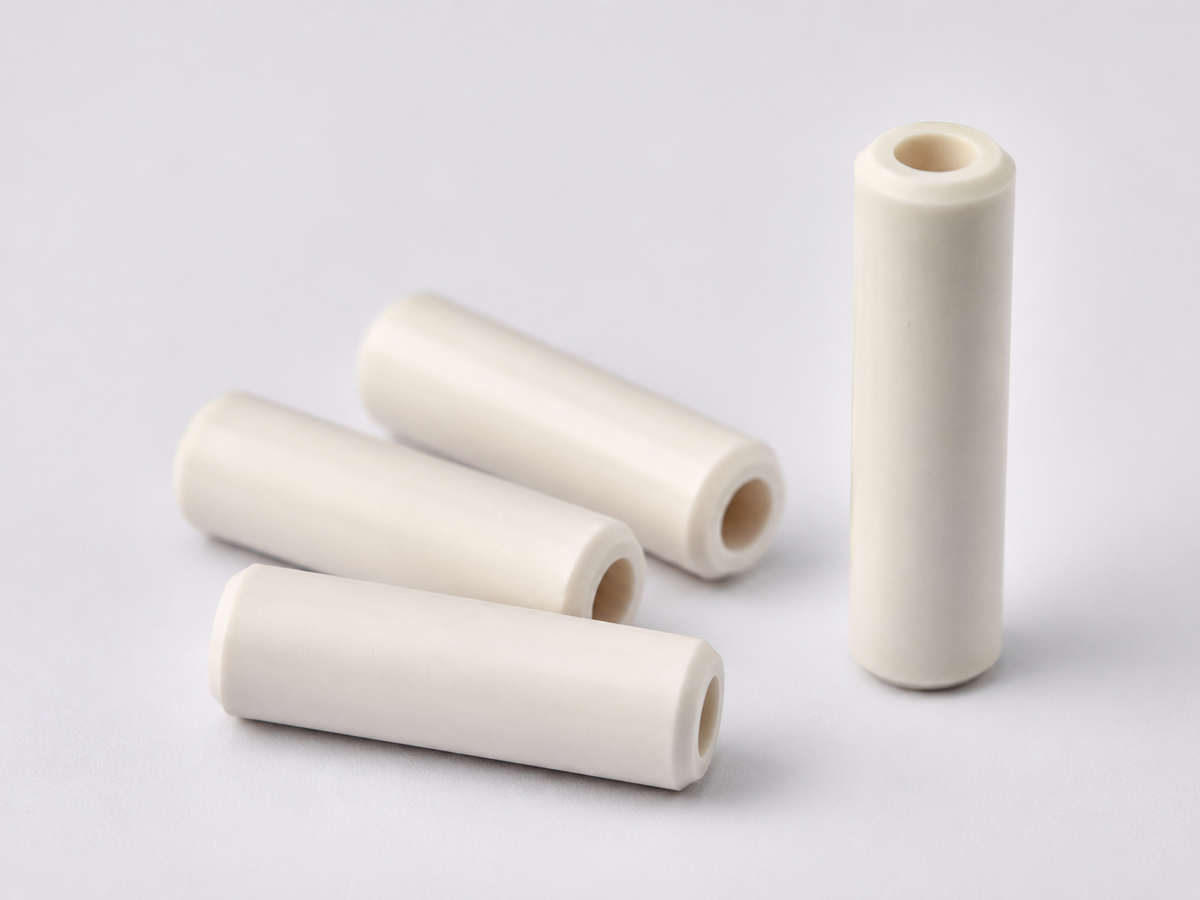
Common parts include ceramic rods, tubes, sleeves, insulators, crucibles, refractory materials, and wear-resistant ceramic components, and they are widely used for semiconductor, electronics, automotive, and aerospace and medical industries.
Different ceramic materials are used for different applications.
| Ceramic Material | Typical Parts | Main Applications |
| Alumina (Al₂O₃) | Ceramic tubes, rods, insulators, crucibles | Electronics, electrical equipment, semiconductor manufacturing |
| Zirconia (ZrO₂) | Structural blanks, sleeves, wear-resistant components | Medical, industrial machinery, precision equipment |
| Silicon Carbide (SiC) | Tubes, mechanical seal blanks, wear-resistant components | Chemical processing, pumps, industrial equipment |
| Silicon Nitride (Si₃N₄) | Rods, rollers, bearing blanks | Automotive, machinery, high-temperature equipment |
| Magnesium Oxide (MgO) | Crucibles, refractory components | Metallurgy, thermal processing |
| Boron Carbide (B₄C) | Wear-resistant and protective components | Industrial protection, abrasive applications |
Cold Isostatic Pressing(CIP) vs Dry Pressing vs Hot Isostatic Pressing(HIP) vs Ceramic Injection Molding(CIM)
| Comparison | Dry Pressing | CIP | HIP | CIM |
| Basic Principle | Pressing powder in a rigid die | Liquid pressure from all directions | High-temperature gas pressure | Injection of ceramic feedstock |
| Pressure Medium | Mechanical punch | Liquid | Inert gas | Injection pressure |
| Temperature | Usually room temperature | Usually room temperature | High temperature | Injection followed by high-temperature sintering |
| Typical Pressure | Around 20–150 MPa, depending on the process | Commonly 100–600 MPa equipment range | Commonly 50–200 MPa | Depends on feedstock and mold |
| Mold | Rigid steel die | Flexible elastomer mold | Encapsulated or suitable preformed part | Precision metal injection mold |
| Density Distribution | May have a density gradient | More uniform | Helps eliminate residual porosity | Depends on filling, debinding, and sintering |
| Suitable Geometry | Simple and relatively flat shapes | Large, thick-walled, and long parts | Parts requiring further densification | Small and complex 3D parts |
| Production Volume | Medium to high | Wet bag: flexible; dry bag: repeat production | Depends on treatment requirements | Medium to high |
| Main Advantage | Fast and economical for simple shapes | Uniform green density | High final density and reduced residual porosity | Complex near-net-shape geometry |
| Main Limitation | Die friction and density gradients | Flexible mold and additional finishing | High equipment and processing cost | Mold cost and complex debinding control |
*The pressure ranges above are general references, not universal industry standards. Actual values vary depending on the material, equipment, and process conditions.
Dry Pressing vs Cold Isostatic Pressing(CIP)
Dry pressing is a common forming method in ceramic manufacturing. Powder is placed into a rigid steel die and compacted using mechanical pressure in one or two directions.
It is suitable for simple shapes, relatively regular dimensions, and high-volume production. Typical products include ceramic plates, spacers, and some electrical insulation components.
The main advantages of dry pressing are high production efficiency and good automation potential. It works well for repeat production.
However, because pressure is mainly applied in one direction, friction between the powder and mold walls can create density gradients. For thicker or high-aspect-ratio parts, this may increase the risk of uneven shrinkage and cracking during sintering.
CIP applies liquid pressure from all directions, helping reduce these directional density differences.
In general, dry pressing is more economical for simple parts with large production volumes. CIP is worth considering when parts are larger, thicker, or require more uniform green density.
Cold Isostatic Pressing(CIP) vs Hot Isostatic Pressing(HIP)
Although CIP and HIP are both isostatic pressing technologies, they serve different purposes.
CIP usually uses liquid pressure at room temperature to compact ceramic powder. Its main purpose is to produce a ceramic green body with uniform density.
HIP uses inert gases such as argon at high temperatures and pressures to further densify materials and reduce internal residual porosity.
Typical HIP pressures range from approximately 50–200 MPa, while temperatures can range from several hundred degrees Celsius to around 2,000°C or higher, depending on the material.
For some high-performance ceramics, HIP can be used after pre-sintering to further reduce residual porosity and improve final density.
Therefore, CIP and HIP are not simply alternatives to each other. Some parts only need CIP followed by conventional sintering, while others may require additional HIP treatment to meet demanding performance requirements.
If you are looking for hot isostatic pressing services, check whether the supplier has the right equipment and experience with your specific ceramic material.
Cold Isostatic Pressing(CIP) vs Ceramic Injection Molding(CIM)
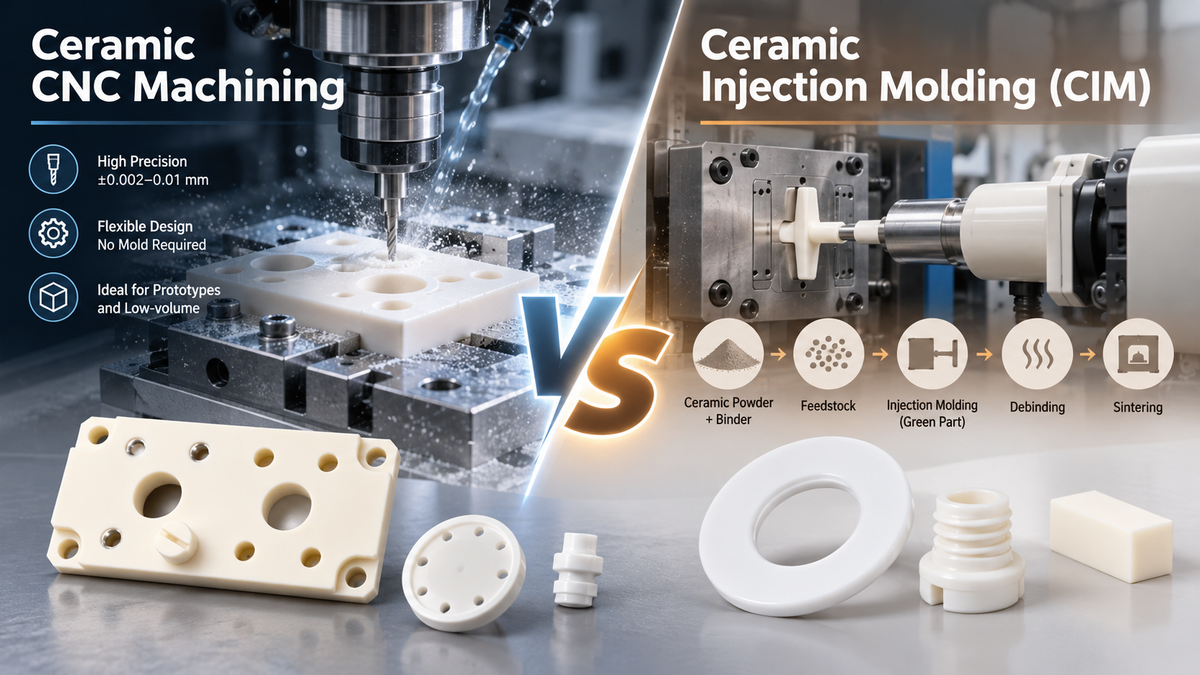
CIM (Ceramic Injection Molding) is a different ceramic forming process. Ceramic powder is mixed with an organic binder to create an injection feedstock. The feedstock is then injected into a precision mold to form the part.
After injection, the part goes through debinding and sintering to obtain its final properties.
CIP is more suitable for large, thick-walled, or relatively regular ceramic blanks. CIM is usually a better option for small parts with complex 3D structures and detailed features.
However, CIM requires precision tooling, which means a higher initial mold investment. For small quantities or simple part designs, CIP or CNC ceramic machining may be more economical.
How to Choose the Right Ceramic Forming Process?
When selecting a ceramic forming process, it is worth considering the following factors.
Part Geometry: Dry Pressing is suitable for simple and regular shapes. CIP is worth considering for large, thick-walled, or high-aspect-ratio parts. CIM is often a better choice for small and complex components.
Material Requirements: Different ceramic materials have different flow properties, compressibility, sintering shrinkage, and final performance. The powder preparation and forming process need to be selected accordingly.
Dimensional Tolerances: If a part has tight dimensional or surface finish requirements, sintering shrinkage and machining allowances need to be considered in advance. Post-processing may include CNC machining, grinding, and polishing.
Production Quantity: For low-volume production and complex parts, tooling investment and unit cost need to be evaluated together. For high-volume production, automation and cycle time become more important.
Final Performance: If a part requires particularly high density or very low residual porosity, further densification processes such as HIP may also need to be considered.
The most important point is not to select a forming process before reviewing the part drawing and application requirements. A good manufacturing solution should meet the required performance and dimensional standards while keeping the overall cost practical.
Partner with XY-GLOBAL for Cold Isostatic Pressing Services
Cold isostatic pressing is shaping ceramic manufacturing by offering superior density, precision and sustainability.
Founded in 2010, XY-GLOBAL brings over 15 years of custom ceramic manufacturing to customers worldwide, delivering desired ceramic components with consisitent quality and required preformance from raw material selection to mass production.
We understand that every ceramic component has different manufacturing requirements. By combining our experience, advanced technology, and engineering expertise, we provide reliable cold isostatic pressing services and make sure each step of the process is carefully controlled for higher quality and efficiency.
Our engineering and sales teams work closely with customers to identify the most suitable ceramic manufacturing process for each project. Our capabilities include:
-
A wide range of ceramic materials to choose from;
-
Custom designs tailored to your specifications;
-
On-demand production with 0 MOQ;
-
Free DFM support;
-
One-stop post-processing, including CNC machining, grinding, lapping, and polishing;
-
Flexible production from prototypes to mass production.
Submit your CAD files for a free DFM review and a competitive quote. Whether you need standard ceramic components or custom parts made through cold isostatic pressing, our team is ready to help you find the right manufacturing solution.
Frequently Asked Questions About Cold Isostatic Pressing
1. Can XY-GLOBAL manufacture custom ceramic parts from customer drawings?
Yes. We can evaluate custom ceramic components based on 2D drawings, 3D models, material requirements, and application conditions. You can also provide critical dimensions, tolerances, surface finish requirements, and estimated order quantities to help us assess the manufacturing process.
2. What information is needed to get a CIP ceramic parts quotation?
The most useful information includes the ceramic material, 2D or 3D drawings, overall dimensions, critical tolerances, required quantity, and application. If the part requires CNC machining, grinding, or polishing after sintering, please include those requirements as well.
3. Can CIP ceramic parts be machined after sintering?
Yes. Depending on the ceramic material and part geometry, post-sintering operations can include CNC machining, diamond grinding, drilling, lapping, and polishing. These processes are often used to achieve tighter dimensional tolerances and better surface finishes.
4. How do I choose between CIP, Dry Pressing, and CIM?
Start with the part geometry and production quantity. CIP is suitable for larger or thick-walled ceramic blanks, Dry Pressing works well for simpler shapes and repeat production, while CIM is often better for small and complex components. XY-GLOBAL can review your drawings and recommend a suitable process.
Делиться:
Metal Injection Molding Medical Parts: Materials, Tolerances and How to Source Them